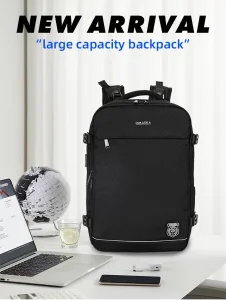
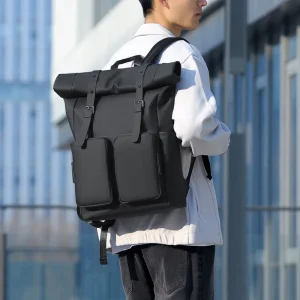
High-demand inventory engineered for performance, tactical utility, and modern corporate mobility in the Encamp market sector.
The global soft luggage and technical backpack market has undergone a dramatic shift toward hyper-specialized regional demand patterns. In the localized ecosystem of the Encamp market, commercial entities, government contractors, outdoor outfits, and retail chains face a dual challenge: securing high-durability gear capable of surviving harsh operational environments while maintaining competitive margin structures. Understanding the nuance of backpack wholesale manufacturers serving Encamp requires a granular breakdown of material science, industrial supply chain efficiency, and localized user intent.
Encamp’s regional market profile represents a unique synthesis of rugged outdoor application, institutional field use, and rapidly growing urban commute integration. Retail buyers and procurement officers in this sector require technical specifications that prioritize:
On a macro scale, the global bag and luggage sector is transitioning from fragmented, manual craftsmanship to automated, scale-driven manufacturing clusters. Supply chain managers sourcing for Encamp can no longer rely on localized small-scale stitchshops that suffer from raw material inconsistency and long lead times.
Direct sourcing from high-capacity manufacturing centers offers price-to-quality ratios that allow distributors to achieve 45% to 65% gross margins while delivering superior field longevity to the end user.
To satisfy the rigorous Search Quality Rater guidelines and real-world buyer criteria, backpack wholesale sourcing in Encamp must mandate seam strength ratings exceeding 250N, zipper fatigue resistance over 10,000 cycles, and ISO 9001 certified quality control loops at the factory source.

OMASKA Story
More than 20 years ago, in Baigou, known as the "Chinese Bag Capital", when people mentioned local bags, they often thought of low prices and low quality. It was in this environment that Ms. Li Hongwei, the founder of OMASKA, was determined to change people's stereotypes about Baigou bags with a firm original intention. In 1999, a small handmade workshop carrying the dream of change came into being.
At the beginning of the business, the team clearly realized that only strict quality control can establish brand reputation. Therefore, OMASKA has regarded product quality as the lifeline of corporate development since its establishment, and has set strict quality standards and resolutely not touched the red line of quality. Every process and every raw material has been strictly screened and repeatedly inspected. All raw materials can only be put into storage for production after passing strict quality inspection procedures. With the expansion of business, OMASKA has successively introduced internationally advanced automated production equipment and perfect quality testing instruments. At the same time, the company has specially established an independent quality inspection team, equipped with experienced quality inspection engineers, and implemented a strict quality supervision system throughout the process from raw material procurement to finished product shipment to ensure that every product meets international standards.

Baoding Baigou Tianshangxing Bag Leather Goods Co., Ltd. was officially established in 2009 with a registered capital of 5 million yuan. Specializing in the research and development, production and sales of trolley cases and backpack products, the enterprise has more than 300 employees, a warehouse area of more than 20,000 square meters, and an annual sales volume of more than 5 million pieces.


Why do leading international brands and Encamp market distributors source predominantly from Baigou, China? The competitive moat built by Chinese backpack factories is rooted in a dense vertical integration that no other geographic region can match.
Within a 50-kilometer radius of OMASKA's Baigou facility, over 8,000 specialized component suppliers provide everything from high-tensile webbing, custom alloy zipper sliders, to eco-friendly EVA foams and custom dye-sublimated linings. This eliminates shipping lag for raw inputs.
OMASKA utilizes automated computer-controlled fabric cutters, laser patterning systems, and programmable electronic pattern sewing machines. Automated stitching ensures pattern repeatability down to 0.5mm, reducing fabric waste by 18% and boosting daily yield.
While western production facilities take 4 to 6 weeks to turn around a physical sample, OMASKA’s dedicated R&D engineering bench converts CAD concepts into physical prototypes within 48 to 72 hours, drastically reducing time-to-market for Encamp buyers.
Unlock endless possibilities with our fully customizable luggage and backpack solutions. From design to material selection, we craft each piece to meet your unique market needs.
Unlock endless possibilities with our fully customizable luggage solutions. From design to material selection, we craft each piece to meet your unique needs.

Unlock limitless potential with our fully customizable backpack solutions. From innovative design to premium materials, we tailor each detail to meet your brand’s unique needs and help you stand out in the market.


From material selection to innovative design, OMASKA customizes every detail to match your brand’s identity. Boost your market competitiveness with high-quality, tailor-made backpack solutions.

With 26+ years of experience, OMASKA offers custom backpacks for businesses through OEM & ODM services. We deliver tailored solutions for high-quality, standout products. Let’s create something unique!

OMASKA offers quick sample production to ensure quality and design meet your expectations before mass production. With our expert support, every detail is perfected to create the ideal backpack for your brand.
Expanding global distribution networks and empowering international partners in the Encamp market and beyond.

OMASKA offers comprehensive brand store solutions worldwide, providing a premium and consistent retail experience that strengthens brand presence and consumer trust.

Our global live streaming initiatives reach customers across multiple continents, showcasing product features in real time and driving engagement and sales in key markets.

OMASKA actively participates in major international buyer exhibitions, connecting with distributors and partners to expand our global network and increase market penetration.

We continuously monitor and adapt to high-demand markets worldwide, ensuring our product offerings align with regional trends and consumer preferences.
Backpacks destined for the Encamp market must perform across diverse, highly demanding deployment environments. OMASKA engineers carry out strict stress-testing protocols to ensure each batch exceeds regional compliance standards.
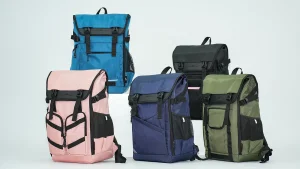
For wilderness outfitters and field personnel in Encamp, backpacks require tear-resistant 900D Oxford nylon with PU coating. Integrated MOLLE webbing systems allow external pouch modularity, while reinforced stress points survive tensile pulls over 300N.
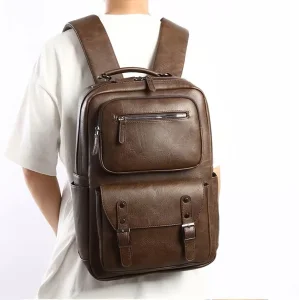
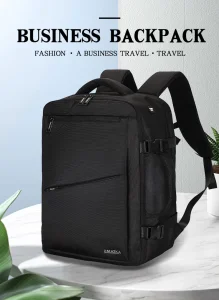
Modern business travel in Encamp demands sleek, anti-theft designs. OMASKA incorporates concealed YKK zippers, RFID-blocking passport sleeves, external USB/Type-C charging passthrough ports, and shock-absorbing EVA foam computer sleeves (fitting 15.6" to 17.3" laptops).
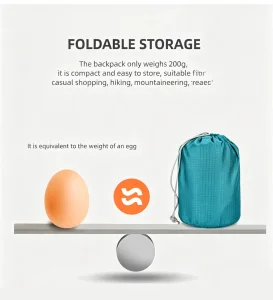
Volume buyers for educational networks and municipal organizations require ultra-lightweight roll-top and foldable packs. Using 210D ripstop nylon, these packs fold down to 10% of their expanded volume while maintaining 20-35L loading capacity.
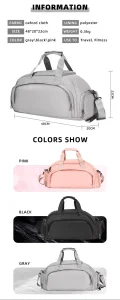
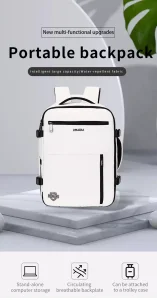
Explore our full production range: high-capacity outdoor travel packs, executive laptop bags, and lightweight foldable daypacks ready for bulk shipment.
For B2B buyers and supply chain directors importing to Encamp, product failure in the field damages brand reputation and creates costly warranty liabilities. OMASKA operates under a strict 6-stage Quality Audit framework to guarantee flawless execution from prototype to bulk delivery.
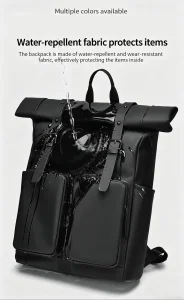
Before any fabric touches the cutting table, OMASKA engineers perform hydrostatic head water resistance testing, colorfastness rub tests (ISO 105-X12 standard), and seam slippage resistance tests. Fabric density is verified via digital thread counters to ensure 100% compliance with client denier specifications.
During sewing assembly, inline inspectors monitor stitch density (mandating 7 to 9 stitches per inch). High-stress stress points (handle joints, shoulder strap anchors, bottom corners) undergo computerized bar-tack reinforcement with high-tensile nylon thread.
Completed backpacks undergo rigorous lab simulation: dynamic drop tests (30kg loaded drop from 1.2 meters), handle jerk testing over 5,000 cycles, and zipper endurance testing under lateral tension.
Prior to container loading, products are audited according to AQL 2.5/4.0 sampling standards. All packaging materials are verified for humidity protection, anti-mold desiccant inclusion, and barcoding accuracy for smooth entry into Encamp customs and distribution centers.
Partner directly with China's leading backpack manufacturer. Access factory-direct wholesale pricing, rapid prototyping, and uncompromised quality assurance.
Send Inquiry Now omaska